MACHINING CASE / 05
Complex 5-Axis Housing.
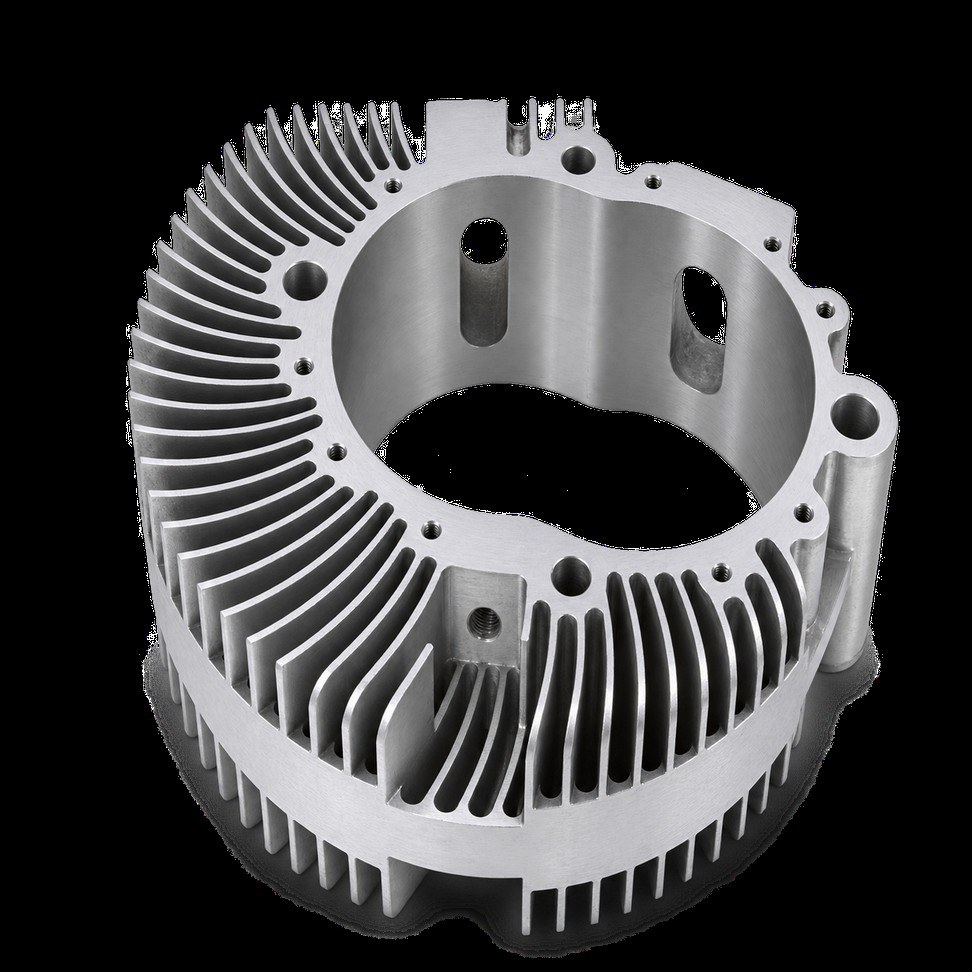
A rotary engine housing combining a non-circular internal profile, thin cooling fins, end faces and intersecting holes.
- MATERIAL
- ZL207 cast aluminium
- FINISH / PROCESS
- Anodised with HVOF bore coating
- REPRESENTATIVE SIZE
- Approx. Ø300 × 110 mm
01
Machining challenges
Distortion control on a casting, datum consistency across a multi-operation route, thin fins that deflect under aggressive cutting, and a hard coating that drives profile-grinding and surface-finish demands — all in one part.MANUFACTURING ROUTE
STEP 01
Casting inspection and ageing
STEP 02
Rough and semi-finish machining
STEP 03
HVOF nickel-based bore coating (0.15 ± 0.01 mm)
STEP 04
Bore profile grinding
STEP 05
Five-axis finishing of fins, end faces and holes
STEP 06
Cleaning
KEY CONTROL POINTS
—
What the route watches
- Common datums across all operations
- Dedicated fixtures per stage
- Coating thickness (0.15 ± 0.01 mm)
- Bore roughness (Ra ≤ 0.12 µm)
- Bore-to-end-face perpendicularity
DIMENSIONAL & SURFACE INSPECTION
—
How it gets verified
- CMM checks on bore profile and end faces
- Coating checks: thickness, roughness, microhardness, porosity, cracks
- Wear testing validated by the customer
The requirements and manufacturing route shown here apply to this project. New components are reviewed against their own drawings and agreed specifications — published values are project-specific requirements, not general capability limits.