MACHINING CASE / 01
RF & Microwave Housing.
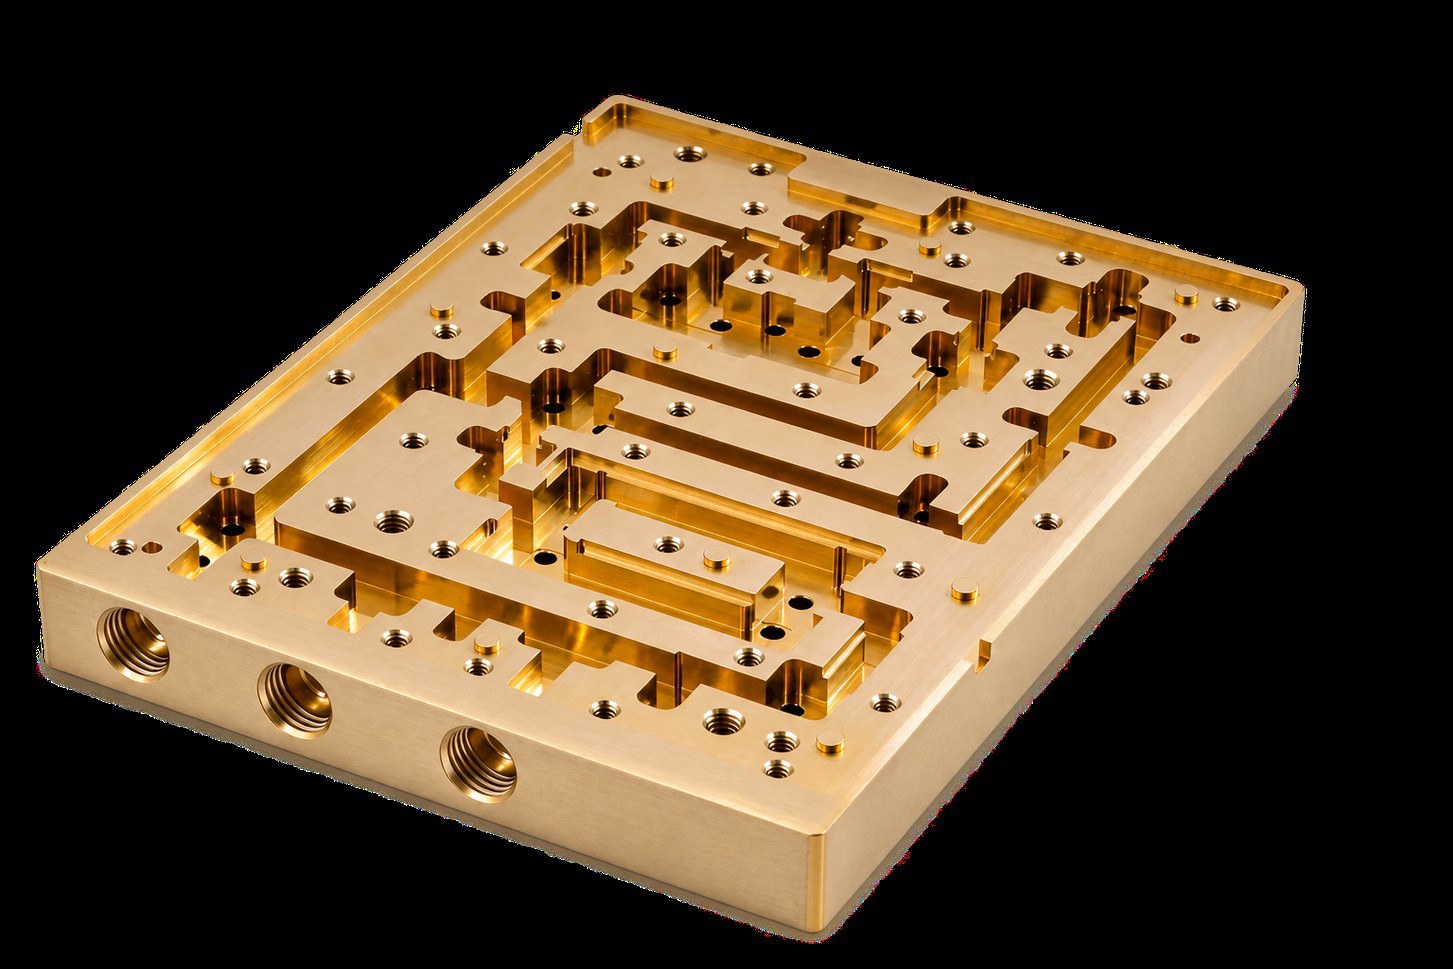
A custom-machined cavity housing for RF and microwave assemblies, combining internal channels, thin partitions, locating features and threaded interfaces.
- MATERIAL
- Brass substrate
- FINISH / PROCESS
- Gold-plated finish
- REPRESENTATIVE SIZE
- 108 × 86 × 16 mm
01
Machining challenges
Narrow, deep internal channels constrain tool access and drive deflection. Thin partitions need deformation control. Channel-wall finish, cover mating surfaces and locating-hole relationships all have to stay consistent — mechanical performance depends on them, even though they never appear in an electrical test.MANUFACTURING ROUTE
STEP 01
Blank preparation and datum machining
STEP 02
Cavity and partition milling
STEP 03
Cover-fixing holes, locating holes, side-interface threads
STEP 04
Deburring and cleaning
STEP 05
Gold plating
STEP 06
Inspection
STEP 07
Protective packaging
KEY CONTROL POINTS
—
What the route watches
- Channel width and depth
- Internal surface finish
- Mating-face flatness
- Assembly parallelism
- Locating-hole position
- Pre-plating surface condition and coating quality
DIMENSIONAL & SURFACE INSPECTION
—
How it gets verified
- CMM dimensional inspection of channels, mating faces and locating features
- Surface roughness checks on channel walls
- Dimensional inspection does not prove RF performance or leak tightness — application testing is scoped separately when required
The requirements and manufacturing route shown here apply to this project. New components are reviewed against their own drawings and agreed specifications — published values are project-specific requirements, not general capability limits.
Related
- Explore cavities & fluid components
- Precision Stepped Shaft — 20CrMnTi, Ø35 × 260 mm